Good shop floor Wi-Fi starts with written requirements, not access point counts. Define what must connect and how fast, survey the building with its machines and racking in place, design for capacity as well as coverage, wire every access point, and separate production, staff, guest and IoT traffic. Then test against your requirements and re-survey whenever the floor changes. This guide walks through each step the way we do it for manufacturers in Kitchener-Waterloo, the GTA and across Ontario.
An office Wi-Fi plan assumes drywall, desks and people who sit still. A plant has none of that. Ceilings are high, steel is everywhere, and the layout changes when a line is reconfigured or a rack moves.
Huawei’s guidance for shop floors notes that large, high areas with metal structures cause high signal attenuation and call for careful antenna choice, with smart antennas recommended for indoor coverage. Industrial planning guidance also says to account for metal, liquids in storage, mezzanines and changing product racks, and warns that moving forklifts can hit and disable wireless equipment.
The stakes are also different. When Wi-Fi drops in an office, people wait. When it drops on a plant floor, scanners stop, handhelds lose work orders and tablets at the line cannot confirm a job. We have covered what that costs in the real cost of downtime for a 50-person shop floor, and it is the reason Wi-Fi deserves its own design, not a few ceiling units added to the office network. For more on the business case, see our note on why managed Wi-Fi matters in manufacturing.
Most failed deployments skip this step. Someone buys access points, mounts them on a grid, and finds out later that the barcode scanners roam badly or the vision system needs lower latency than Wi-Fi was giving it.
NIST’s guidance on factory workcell wireless requirements says to establish measurable targets for latency, reliability, scale, range, payload size and update rate that reflect current and future needs. Translate that into a short table for your own plant:
| Application | Typical devices | What to define |
|---|---|---|
| Handheld scanners and mobile computers | Scanners, rugged tablets | Roaming behaviour, coverage in every aisle, battery impact |
| Machine connectivity and monitoring | Gateways, sensors, HMIs | Reliability target, update rate, whether a cable is the better choice |
| Vision, quality and traceability | Cameras, inspection stations | Bandwidth per device, latency tolerance |
| Voice and messaging | Wi-Fi phones, radios | Continuous coverage, no dead spots at doors and docks |
| Staff and guests | Laptops, phones | Separate network, bandwidth limits |
| Future growth | New lines, AGVs, more sensors | Extra capacity, spare cable runs |
Every row should have a number beside it. “Reliable” is not a requirement. “No scanner drop longer than a few seconds anywhere in receiving” is one.
IBwave’s manufacturing Wi-Fi guidance adds the planning inputs: services, application types, data segmentation, building parameters, density and future connection capacity. Be honest here about which machines should not be on Wi-Fi at all. Safety-related and tightly timed control traffic often belongs on cable.
If you want an outside view of where your plant stands before you start, our manufacturing IT assessment for Ontario plants is built for this stage.
NIST’s lifecycle guidance recommends a factory survey that identifies all machines, processes, programs and applications, and reviews the physical layout and materials. It also notes that organizations may lack complete awareness of factory operations, which are often captured in paper blueprints that are hard to analyze.
That matches what we see. Floor plans are out of date. A wall has moved, a mezzanine was added, a new press now sits where the drawing shows open space. So the survey has two parts:
Then build a predictive model: a floor plan loaded into a design tool, with walls, racking and machinery drawn in, so you can place access points on screen before drilling anything. Predictive models are a starting point. Confirm them with a pre-deployment measurement using a test access point at real mounting height, especially in the worst areas such as dense racking or near large machinery.
Also check for outside interference. Neighbouring tenants in an industrial park, wireless equipment from other systems and microwave sources can all share your spectrum.
Coverage means you can see a signal. Capacity means everyone on it can get work done at once. A plant can have full signal bars and still be unusable if forty scanners, thirty tablets and a pile of sensors contend for the same channel.
Plan these elements together:
Warehouse design specialists list the recurring traps: inaccurate floor plans, layer-one interference, metal reflections and multipath. Multipath is signal bouncing off steel and arriving at the device several times, which is why more power rarely fixes a metal-heavy area. Better placement does.
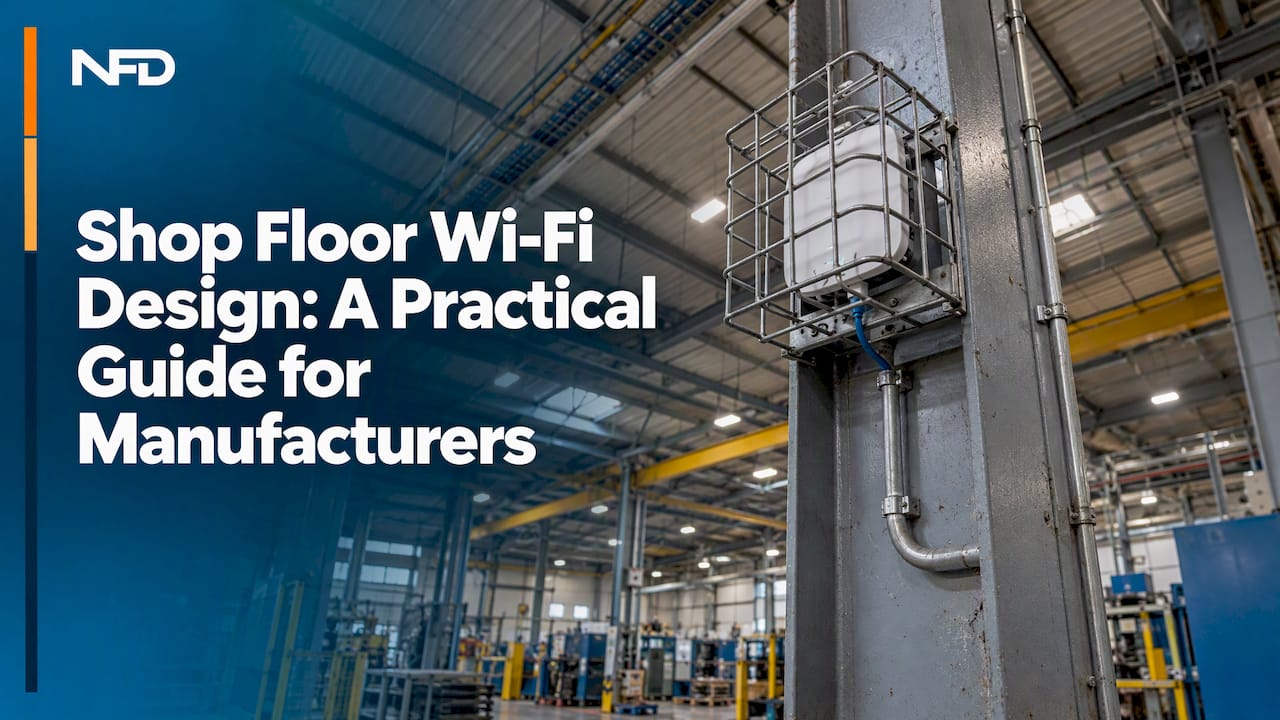
Every access point should have a cabled connection back to the network. Wireless backhaul between access points halves available capacity and adds failure points, so reserve it for places where cabling is truly impractical.
A few build details save repair calls later:
If your plant has several buildings or sites, the same discipline applies between them. Our guides on multi-site network design for SMBs and networks for multi-site business cover that side.
A single flat Wi-Fi network for everything is the most common weakness we find. A guest phone, an office laptop and a machine gateway should not share a broadcast domain.
The Canadian Centre for Cyber Security recommends WPA3 for new deployments if available, separate security zones using SSIDs and VLANs, and client isolation. It says IoT devices should be isolated from employee and guest networks, that WEP can be easily compromised and that WPA1 should be avoided where sensitive information is handled.
A workable layout for most plants looks like this:
| Network | Who or what | Controls |
|---|---|---|
| Corporate | Staff laptops and phones | Strong authentication, access to business systems |
| Production mobile | Scanners, rugged tablets | Access only to the MES, ERP or WMS servers they need |
| IoT and machine | Sensors, gateways, cameras | Isolated, no internet unless required, no access to corporate |
| Guest | Visitors, drivers | Internet only, bandwidth limits, isolated clients |
Some older handhelds only support older security modes. Put them in their own network with tight firewall rules and a replacement date, instead of weakening the whole plant. Camera traffic deserves its own VLAN too; see our camera network VLAN setup guide.
Protect the people who manage the wireless system as well. Administrator access to controllers and cloud dashboards should require multi-factor authentication, and phishing-resistant options such as hardware security keys for MFA are worth considering for those accounts. Keep firmware current, since the Cyber Centre lists unpatched firmware among the first Wi-Fi threats to address.
Wireless sits next to production systems in a plant, so it also helps to read the Cyber Centre’s overview of security considerations for industrial control systems, which introduces how to protect the layer that runs your machinery. Our own explainer, industrial network security for IT managers, and our manufacturing cybersecurity best practices take it further.
For very large sites or demanding mobile applications, some manufacturers look beyond Wi-Fi. Innovation, Science and Economic Development Canada notes that private networks let organizations control data, services, policies and security, and can support asset tracking and automated vehicles in manufacturing. For most small and mid-sized plants, a well-designed Wi-Fi network remains the practical choice. Revisit the question when your requirements table shows needs Wi-Fi cannot meet.
A design is not finished at installation. NIST advises an iterative approach and validating performance against the original requirements and design intent. That is why Step 1 matters: it gives you something to test against.
After installation:
Treat any layout change as a trigger: a new line, a taller rack, a relocated dock door, a new group of devices. A quick re-survey is far cheaper than a week of unexplained slowdowns.
We see the same pattern in plants across Kitchener-Waterloo and the GTA. Wi-Fi is installed once, grows by accident, and nobody owns it until it fails during a shift. Our view is that wireless on the floor should be managed like any other piece of production equipment: it has requirements, a maintenance schedule, a monitored state and a named owner.
That is why we handle monitoring, security and helpdesk together. When a scanner problem is really a channel conflict, or a flaky handheld is really a segmentation rule, one team sees the whole picture and nobody waits on a third-party vendor to point at someone else. We also explain findings in plain language, so a plant manager can decide what to fund first without decoding RF jargon.
If you only do three things this quarter, write down your requirements, survey the floor as it is, and isolate IoT and guest traffic from everything else.
— Geeshan
NetFusion Designs is a SOC 2 Type II certified managed IT provider serving manufacturers across Ontario, with teams in Kitchener-Waterloo, Toronto, Markham and Mississauga, and a 24/7 NOC. We can assess your current wireless and network setup, help you define requirements, and then run the network with monitoring, security and helpdesk under one agreement. If you already have an IT person, our co-managed model lets us cover the parts you need.
Start with our Managed IT Services page, or ask for a manufacturing IT assessment of your plant. If you are in Waterloo Region, see managed IT in Kitchener and Waterloo.
There is no honest number without a survey. It depends on ceiling height, racking, machinery, the number of devices and what they do. A predictive model followed by test measurements in the hardest areas gives you a defensible count before you buy.
For new installs, yes, it is a sensible baseline. Huawei cites a four-fold throughput and capacity improvement over the previous generation. Your gain depends on your client devices, so check which handhelds and tablets support it.
Put tightly timed or safety-related traffic on cable. Wi-Fi suits mobile devices, monitoring and many sensors. Set measurable latency and reliability targets first, as NIST recommends, and let the numbers decide.
Run a survey after any significant change to layout, racking, machinery or device count, and schedule periodic checks even when nothing seems to change. Monitoring dashboards help you spot interference shifts between surveys.